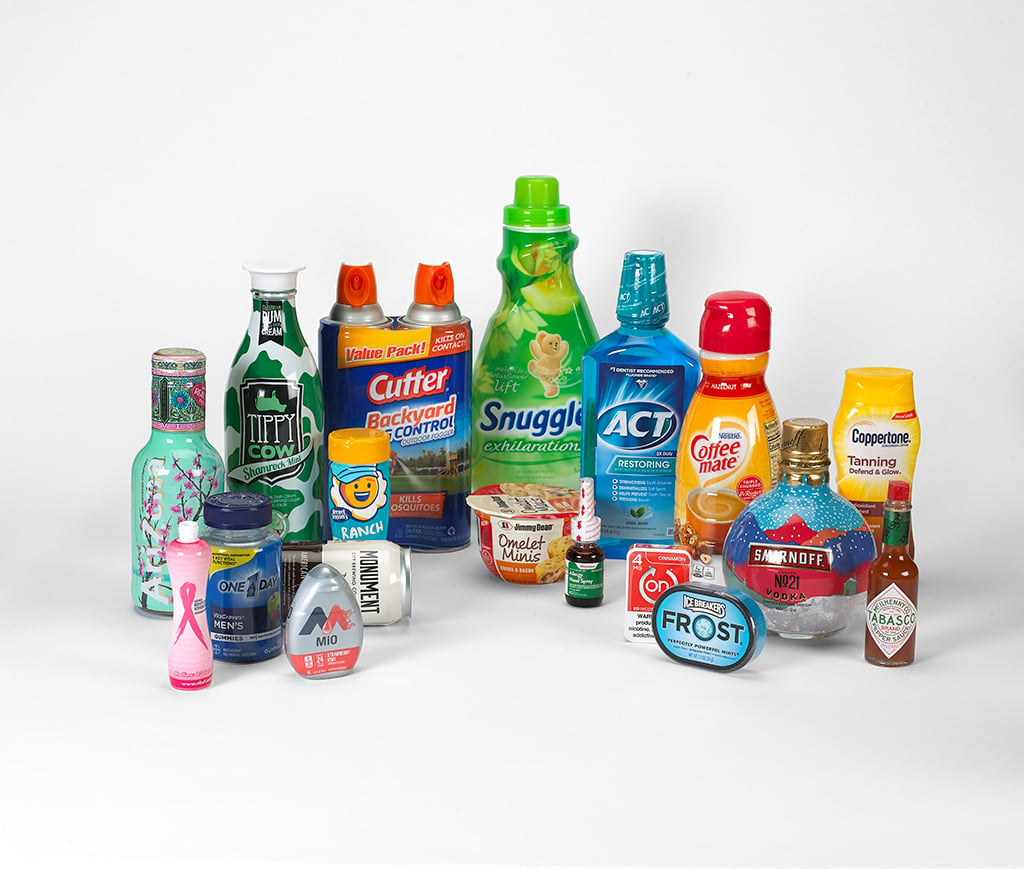
Today's shrink sleeve labeling machinery is designed to run efficiently and exhibit a long life cycle. Over time, however, you may encounter some issues with your machine, and in some cases, this may relate to the materials you are using. To help you out, we've provided a guide on how to troubleshoot labeling issues with your shrink sleeve machinery.
1. Run New, High-Quality Labels
One way to narrow down whether the performance issues with your shrink sleeve labeling machinery are caused by the machine itself, or the labels you are using, is to run the machinery using a roll of labels that you know run well. Ensure that these labels are the right size and are not damaged in any way. If the machine functions properly using these labels, you know the problem lies with the film material you are using and can then more easily identify and troubleshoot the issue.
2. Check the Lay Flat
It's important to understand the tolerances of your shrink sleeve materials and ensure that the lay flat dimensions (the measurement, in millimeters, across the flattened tube) of your labels fall within those tolerances. Have a millimeter scale near the machine and instruct the operators how to measure the lay flat dimensions of your labels. If the labels are outside the specified tolerances you will encounter problems.
3. Check for Split Seams
Make sure that seam on your label is correctly positioned and does not split open due to lack of solvent adhesive. Seams should be consistent and intact, with no excessive solvent welding the inner surface of the sleeves together.
4. Check for Roll Damage Caused by Overheating
Shrink labels can become deformed by overheating in transit or storage. If your labels seem crinkled, warped, or deformed in any way, they may have become overheated and will not apply properly. Damaged labels will jam when running through the shrink sleeve machinery. Make sure your sleeves are stored at the temperature required by your sleeve supplier. Bring rolls to the line only as needed, particularly if the plant is not air conditioned.
5. Check the Dates on Your Labels
Shrink labels have a shelf life and you should be aware of labels that have expired. Labels that are older than 9-12 months begin to lose their functionality and they may cause your shrink sleeving machinery to malfunction. Check with your label supplier for the best dates of use. Discard labels that have expired by more than a month or two.
6. Clear the Tunnel and Applicator of Excess Material
If excess material such as loose sleeves or fallen containers has gathered in the tunnel or applicator of your shrink sleeve labeling machinery, make sure to thoroughly clean it out. The machine and tunnel will perform better once this debris has been cleared out. Make sure the conveyor is clean and running smoothly, without hesitating.
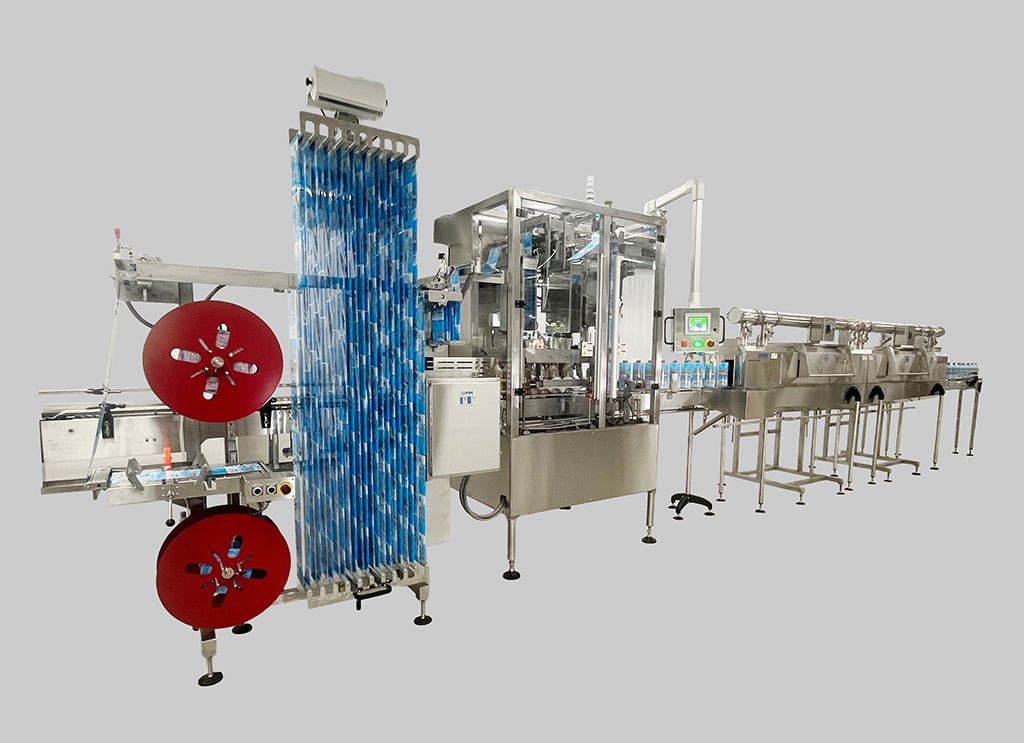
7. Confirm Conveyor Speeds in the Operator's Manual
If your shrink sleeve labeling machinery is malfunctioning, you may be running the conveyor at the wrong speed. Check the recommended speed in your operator manual, then measure the speed of your conveyor using a tachometer that is designed for measuring conveyor speeds. If the speed is above or below what it should be, adjust as needed and run the machinery again. Conveyor speed can not only affect sleeve application, it determines how long the product is in the shrink tunnel, which affects the shrink quality and appearance of your products.
8. Check to see if the Chain is too Hot
If the chain on your machine is overheating, it may cause problems such as shrinking the film on the label prematurely. An overheating chain is evidence of other issues within your machine that will need to be addressed before you continue running it. There are methods of cooling the chain, such as adding a blower in the body of the conveyor to dissipate heat.
9. Check the Edges of the Film for Damage
Damage can occur on the edges of the film while it is still on the roll due to improper handling or stacking. Damage on the edges can cause film jams during application, and show up in holes in the shrink film on your product. Proper storage practices are necessary to ensure smooth application and flawless final appearance.
10. Remove Fans from the Shrink Tunnel Area
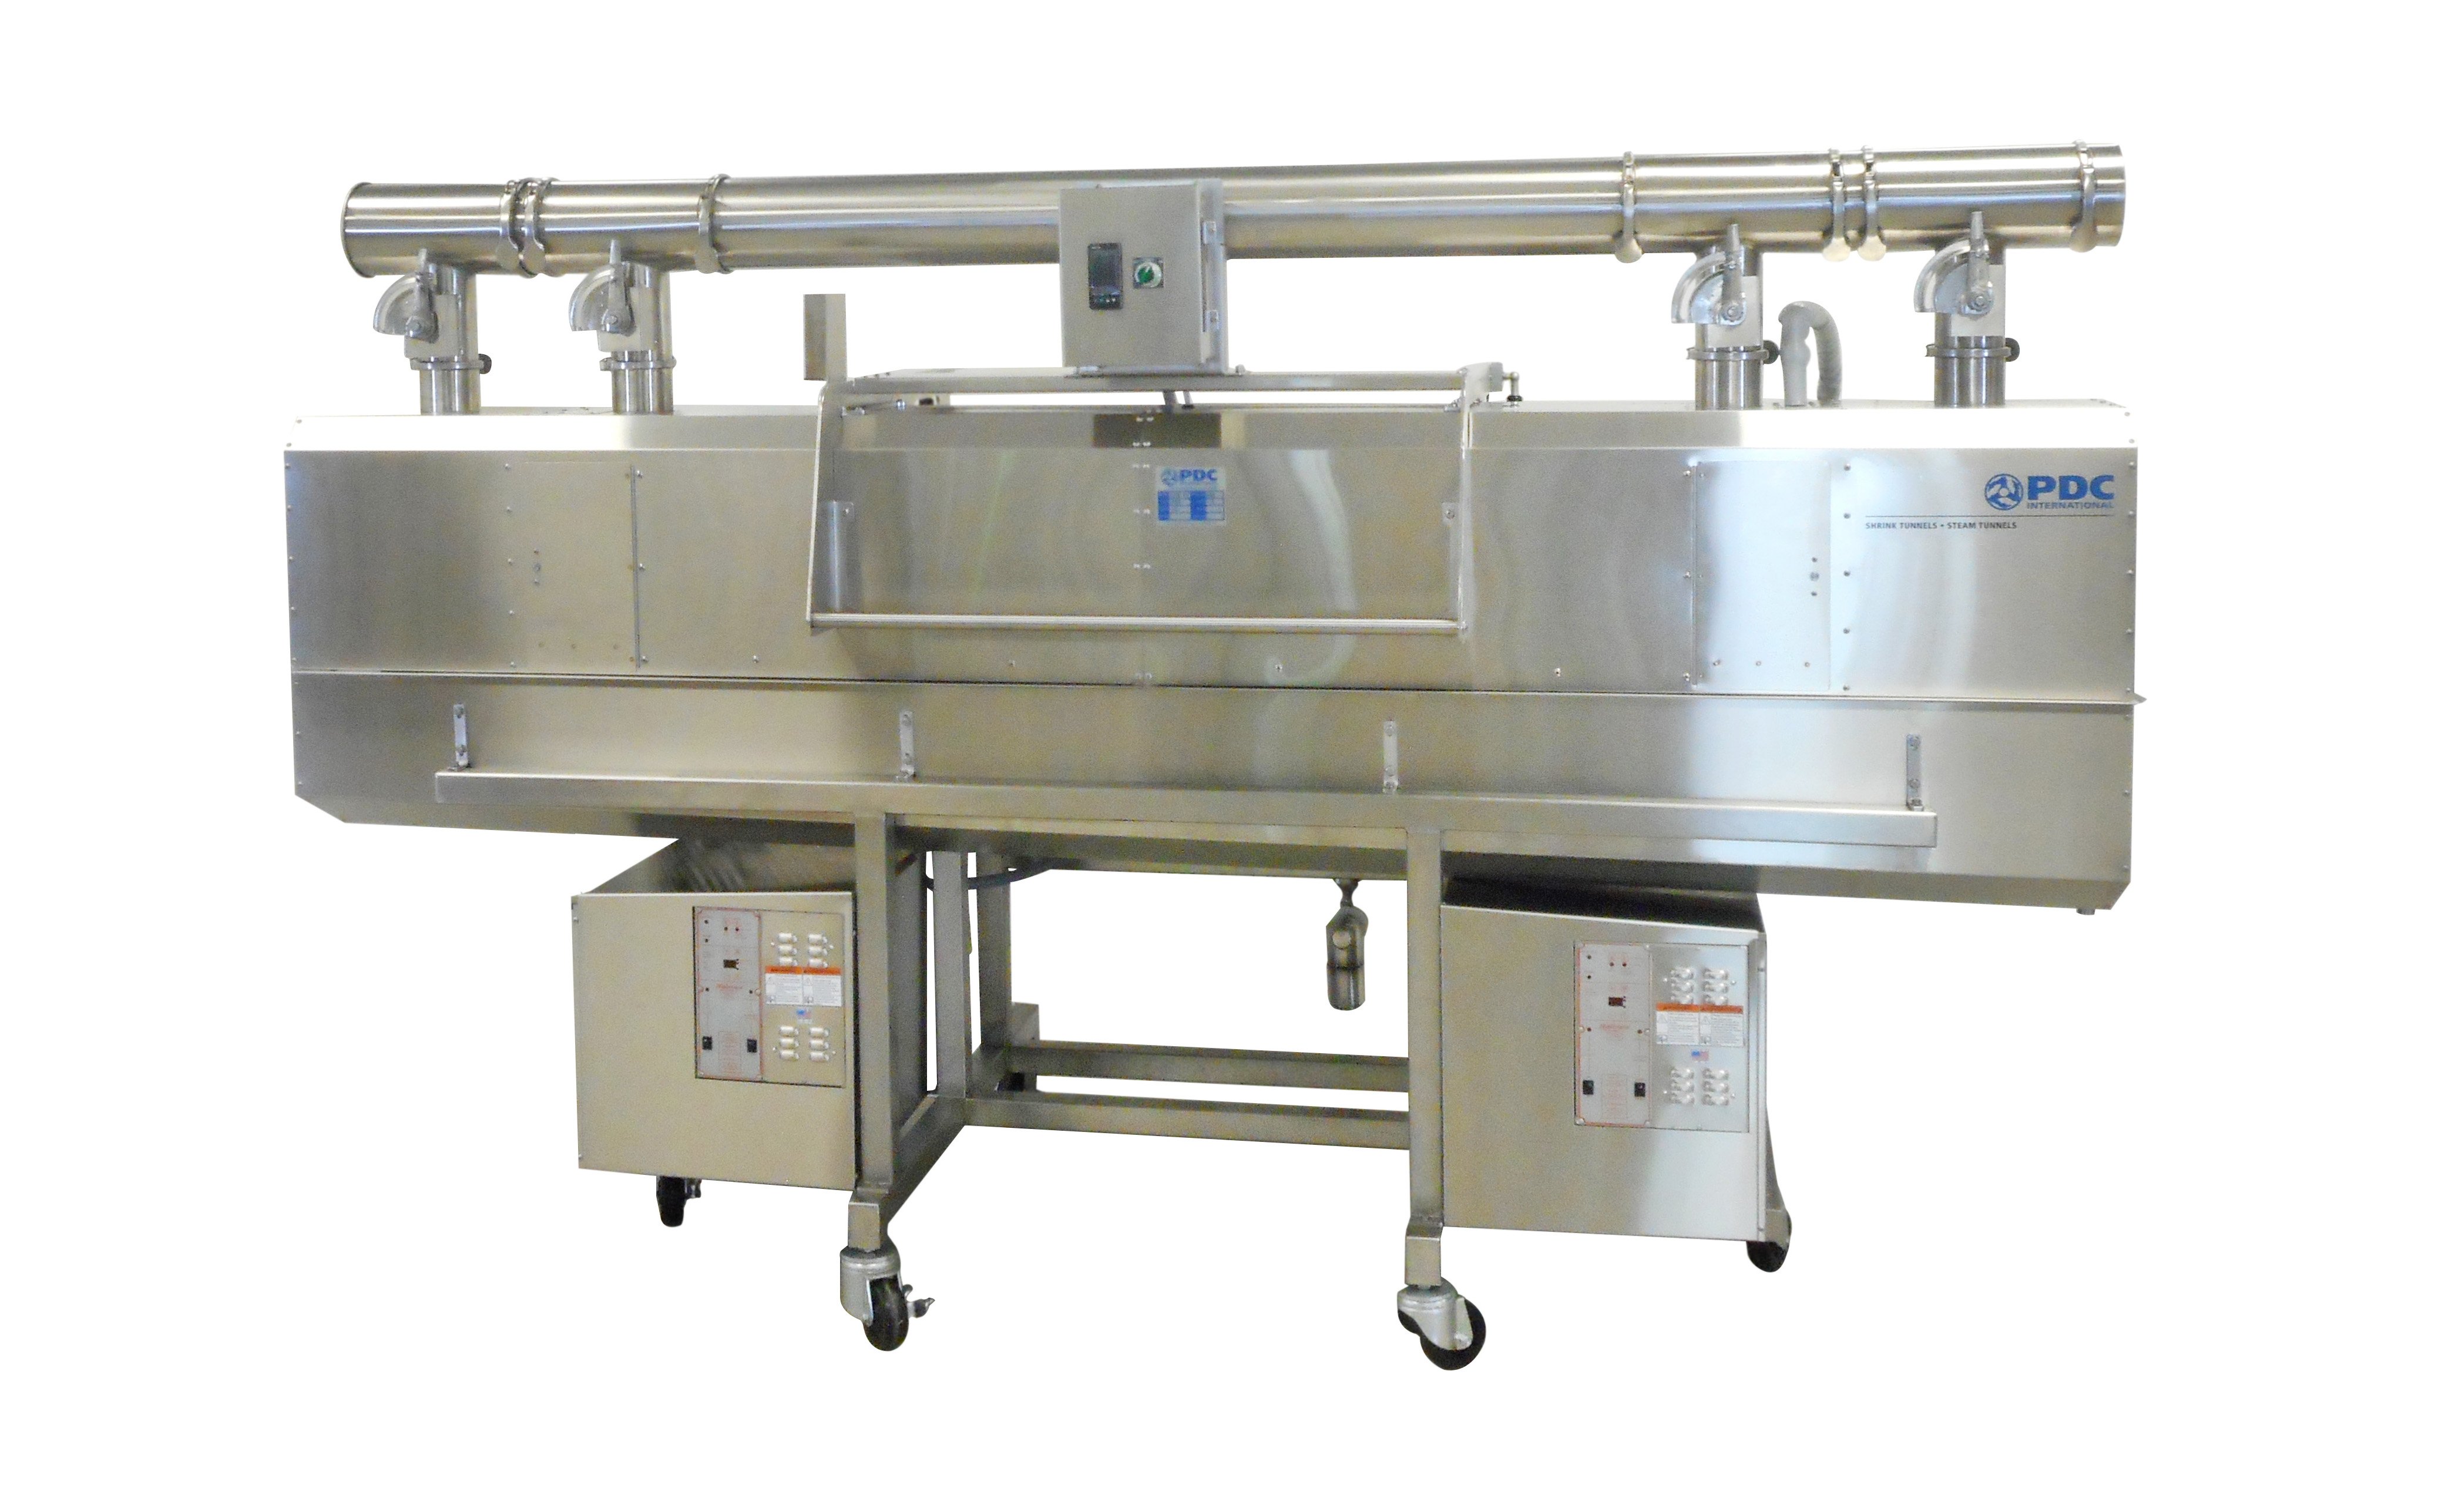
Air flow from fans near a shrink tunnel can cause the shrink tunnel to fluctuate in temperature, creating variation results. The difference between 5 degrees can mean the difference between a good and a bad product. A fan placed in the tunnel's vicinity can sway the tunnel temp enough to impact the shrink quality and consistency.
11. Check the Location and Height of Sensors
Make sure your sensors are aligned and in the correct location for proper sleeve or band application. Sensors are employed for a number of reasons from sleeve application timing, to determination of the correct location of the film on a product. On the application side a product seen by the sensor will trigger the film to be shot on the product. A sensor in the wrong location will cause jams from early or late application of the film. Post application, sensors can confirm the correct location of the film before entering the shrink tunnel. Coupled with a reject / eject system, the non conforming products can be kicked off the line for rework.
12. Know what Shrink Film you are Running
There are many types of shrink films on the market. Each film has its own physical and performance attributes. For example, a change from PET to CPET, a more recyclable film, would most likely not run on the same tunnel settings. Just because it looks the same doesn't mean it will react the same way. Check the core tags on the film to make sure you are using the same film roll after roll, lot after lot.
13. Check your Steam Tunnel Blower Speed
Many steam tunnels have a blower fan that evacuates the steam on the interior of the tunnel in a controlled manner. If the blower setting is too high, excessive steam will be sucked out of the tunnel, resulting in poor shrink results. On the other hand, if the blower speed is too slow, steam will billow out of the entrance and exit of the tunnel. There is an ideal midground when dealing with blower speeds, and it has a direct impact on the shrink quality and tunnel performance.
14. Check the you Shrink Tunnel Height
Most hot air tunnels have an adjustable height whether it is a hand crank, or motorized actuator. A tunnel that is too high could pull the shrink sleeve higher on your product, and not cover the bottom of your product. A tunnel that is too low may cause the shrink at the top of the sleeve to be unfinished. An adjustment of even 1/4 inch can have a major impact on the final shrink appearance.
15. Check Steam Tunnel Interior Pipes
Depending on your water hardness, minerals in the water can calcify on your internal steam pipes, blocking the steam holes over time. Clear out the holes gently with a drill bit by hand. Or replace the pipes if they are corroded.
The Importance of High-Quality Shrink Sleeve Machinery
Having your operation stalled by issues with your shrink sleeve labeling machinery can be costly. That's why it's important to ensure you are using high-quality labels as well as high-quality shrink sleeve labeling machinery.
At PDC, the packaging machinery that we manufacture is robust in design to function reliably for decades, helping you avoid costly malfunctions and downtime. PDC cutting blades are the most rugged in the industry, and last months, not days. If you would like to learn more about putting our high-quality shrink sleeve labeling and tamper-evident banding machinery to work in your plant, we invite you to contact us today. We look forward to working with you.


 © PDC International Corp. 2026


